Electric-hydraulic CNC press brake
The electric-hydraulic press brake drives the main oil pump with a servo motor instead of an asynchronous motor. The ram synchronisation, the approach speed and the energy bill all change for the better — and the control is a Delem DA53T running Y1/Y2 plus two auxiliary axes.
Why a servo-driven pump changes the machine
- The controller can control the Y1 and Y2 axes (Y1 controls the left cylinder and Y2 the right) to ensure synchronous movement of the ram — no torsion shaft needed for cylinder sync.
- Quiet speed waiting and fast down, about 25 decibels; low noise during pressing and return.
- The pressure in the hydraulic system is the closed-loop control of the servo main motor.
- The main oil pump does not apply work under the drive of the servo main motor, and energy consumption is 60% lower than that of a general CNC press brake machine.
Machine construction
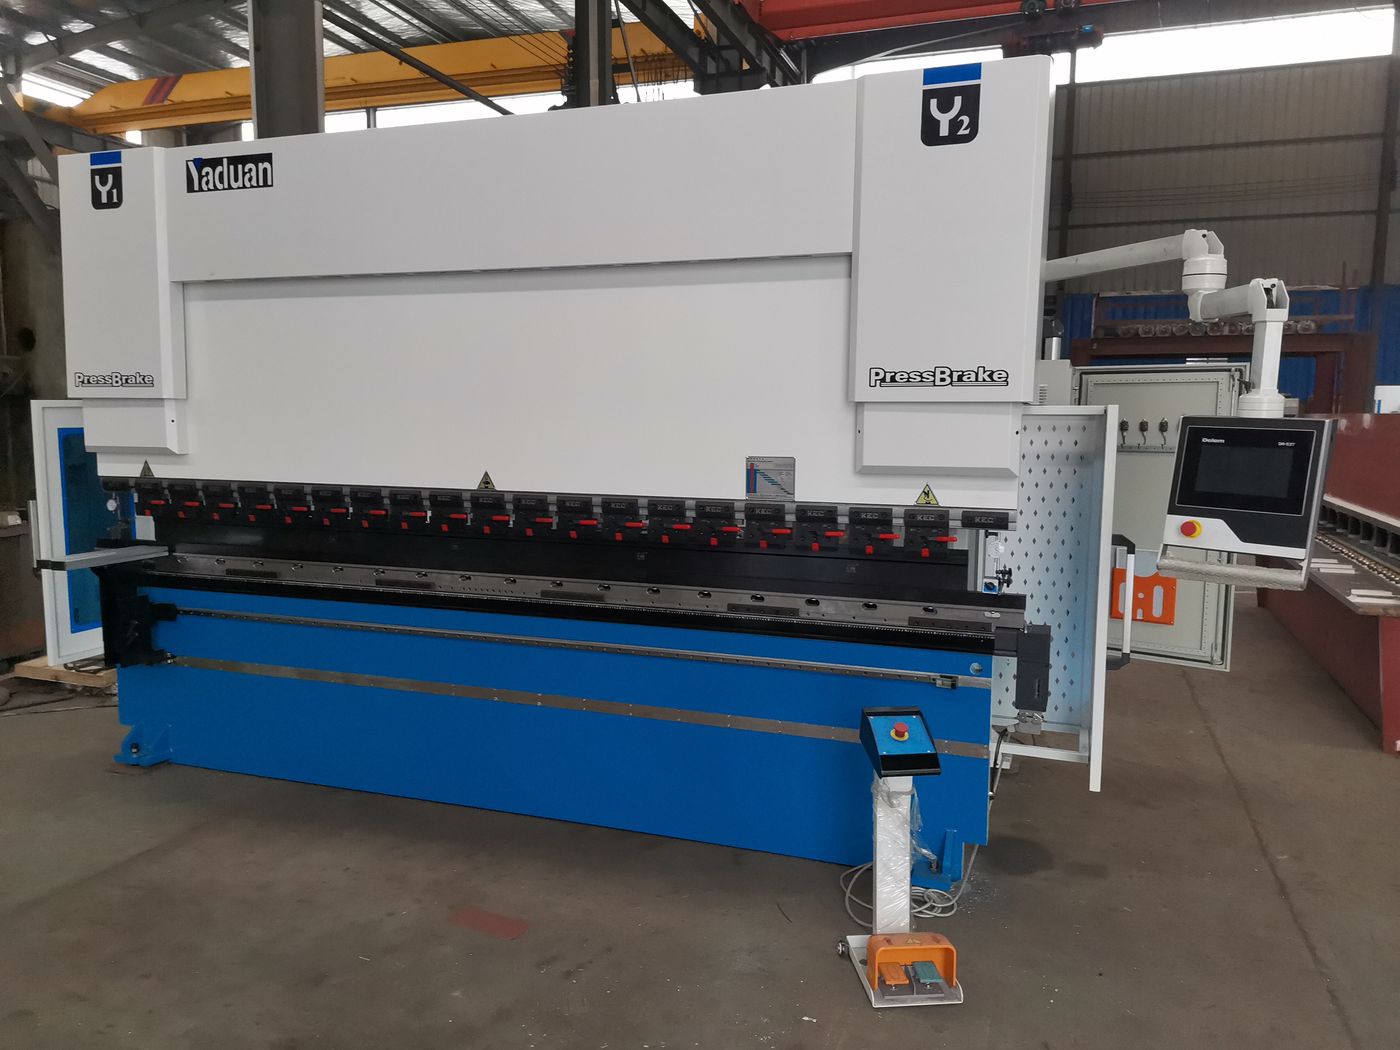
- New EU streamlined design.
- The whole frame of the press brake adopts integrated welding, and is tempered to eliminate internal stress.
- Shot blast to remove rust and sprayed with anti-rust treatment.
- The frame is formed by the imported CNC three-dimensional machining centre in one process, which ensures the parallelism and verticality of each mounting surface.
Delem DA53T control system
- "Hot-key" touch navigation, 10.1" high-resolution colour TFT
- Up to 4 axes (Y1, Y2 + 2 auxiliary axes)
- Crowning control; tool / material / product library
- Servo and frequency inverter control
- Advanced Y-axis control algorithms for closed-loop as well as open-loop valves
Working features
- Fast clamp and die holder — replace the top punch in very short time; the die holder makes die changes smooth and fast.
- Fast intermediate loading and unloading function to improve work efficiency.
- South Korea foot switch — lengthened service life and improved operation.
- Mechanical crowning system — the motorised crowning system adjusts the parallelism and straightness automatically.
- Front support arms — 180° adjustable, with two linear guides to keep heavy-duty plate working.
Press brake toolings
The standard top punch and dual-V bottom die are specially designed for bending sheet metals. More press brake toolings can be selected as per your practical use. Material and HRC47 degree values are marked on each piece.
Back gauge and electrics
- Double guide rails — more convenient to use and stronger load-bearing capacity.
- Back gauge system — HIWIN ball screw and linear guide CNC backgauge for 4+1 axis; the Z stopper and X axis are controlled by servo motor on HIWIN ball screw and linear guide.
- Schneider electrical — high-quality electric parts keep the machine performing well even where the electricity is not stable, and replacements are easy to get anywhere in the world.
Representative specification
| Parameter | WC67K 110T 4100 |
|---|---|
| Nominal pressure | 1,100 kN |
| Worktable length | 4,100 mm |
| Distance between columns | 2,600 mm |
| Throat depth | 350 mm |
| Ram travel | 150 mm |
| Control | Delem DA53T, 4+1 axis |
| Main drive | Servo main motor + servo pump |
Other tonnages, bed lengths and axis configurations are built to order.
Ask about the electric-hydraulic cnc press brake
Send the part you need to bend and we will come back with a configuration and a quote.